


Hebei Juliang Technology Co., Ltd. is one of the leading manufacturers and suppliers of compact plasma gantry cutter in China. Please feel free to buy CE approved machinery made in China here from our factory. All customized machines are with high quality and competitive price.
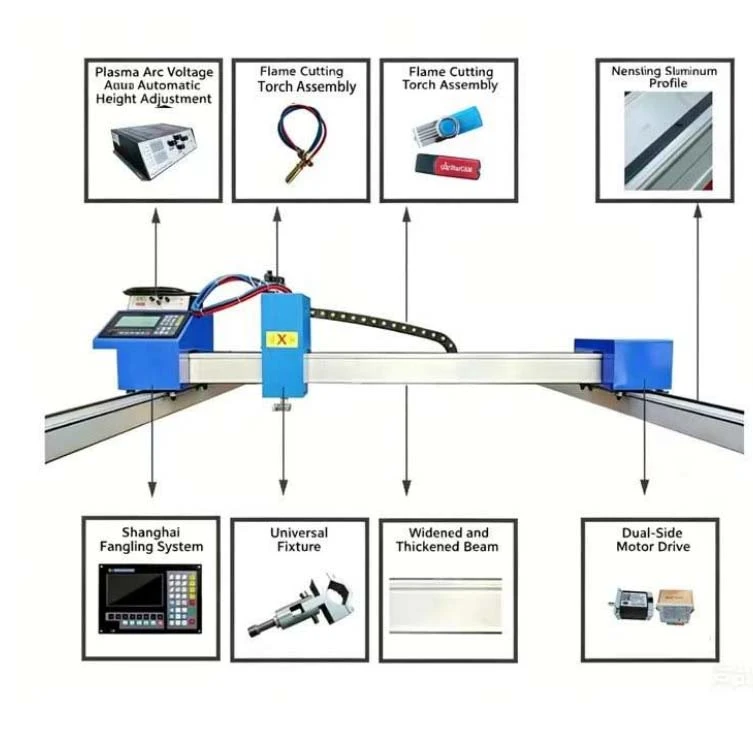
A Compact Plasma Gantry Cutter is a CNC-controlled thermal cutting system that uses an overhead bridge-the gantry-to move a plasma torch across a stationary cutting table-. Unlike smaller table-type machines where the material moves, the gantry moves over the material. You load a full sheet of steel or metal plate onto the table, the machine follows a programmed path from your CAD drawing, and you get consistent, repeatable parts without repositioning.
The "compact" part means the machine is designed to fit in workshops where floor space is tight-typically occupying about 2–3 square meters while still handling standard sheet sizes. This is not a full-size industrial gantry system that takes up half a workshop. It's a machine built for small fabrication shops, garages, and light production environments.

Setting up your compact gantry system is straightforward
1.Unpack and inspect: Carefully check the contents for any shipping damage and ensure all parts are accounted for.
2.Assemble the frame: Many compact systems use simple bolt-together frames. Refer to the assembly guide. Some units arrive already put together.
3.Install the rails: Attach the rails to the frame, making sure they are perfectly parallel and level. Any slight angle can cause the gantry to get stuck.
4.Mount the gantry: Position the gantry onto the rails. You might need to adjust the wheel tension so it glides smoothly.
5.Connect the torch: Secure the torch to its carriage and hook up the torch cable to the plasma power source. Don't forget the ground clamp.
6. Install the software: Load the control software onto your computer and connect the controller using the USB cable. The system handles standard file types and includes nesting tools.
7.Calibrate: Perform the calibration steps and check that the axes move correctly. Make sure the torch activates as expected.
8.Test cut: Before diving into production, run a test cut on some scrap metal.
Expect to go from delivery to your first cut in about 2-4 hours for initial setup.
trouble shooting
Inconsistent cut quality often stems from worn consumables like the electrode and nozzle. Replacing these, along with ensuring proper air pressure (too low hinders arc penetration, too high causes excess dross), should help.
Arc instability can be due to worn consumables or air line moisture. The electrode's hafnium insert wears down, so replace it when the pit is deep. Check your air dryer, as moisture significantly damages consumables.
Excessive dross usually means incorrect cutting speed, high current, or improper gas pressure. Start by inspecting the nozzle, then verify your cutting speed matches the recommended settings for your material and thickness.
If the machine overheats, check the duty cycle. Exceeding it will cause the machine to shut down for protection. Allow it to cool and clean the air intake filter.
Gantry binding occurs when rails are misaligned or gantry wheels need adjustment. Verify rail alignment and adjust wheel tension.
Maintenance and consumables for compact plasma gantry cutter
Daily:
Check torch consumables (electrode, nozzle, swirl ring, shield cap) and replace if worn.
Inspect the ground clamp and clean the rails.
Weekly:
Clean the torch body.
Verify all cable connections are secure.
Lubricate rails and drive components.
Monthly:
Replace any consumables showing wear.
Check the electrode's pit depth.
Ensure the nozzle orifice is still round.
Clean the gas filters.
Consumables Details:
The electrode's hafnium insert wears down over time. Replace it when the pit depth is around 1.6mm. The nozzle orifice can also wear and become misshapen, affecting cut quality, so replace it when you notice a drop in performance. For optimal results, change both the nozzle and electrode at the same time.

Common Problem
Does the Compact Plasma Gantry Cutter require a special foundation?
No. Compact gantry systems are light enough to be installed on a level workshop floor. No special foundation is required. Level the machine using the adjustable feet.
Can I cut parts that are larger than the cutting table by repositioning the material?
Yes, you can cut larger parts by repositioning the material. The CNC controller supports program splitting and repositioning, but this requires careful alignment and may introduce inaccuracy. For best results, repositioning should be avoided where possible. If you frequently cut oversized parts, consider a larger machine with a longer rail length-the gantry design supports extension up to 20 meters or more.
How does the machine handle cutting stainless steel and aluminum without damaging the torch?
The plasma torch operates the same way for all conductive metals, but gas selection matters. For stainless steel, nitrogen or argon-hydrogen mixtures give better edge quality than air. For aluminum, use nitrogen to prevent oxidation. The plasma power source supports dual gas connections, so you can switch between gases without changing the torch. Always use clean, dry gas-moisture damages consumables.
Can the machine be used for both manual and automated cutting?
Yes, the machine supports both modes. In manual mode, you can move the torch using the pendant or joystick for simple cuts. In automated mode, the CNC follows programmed paths from your CAD files. Most operators use the machine in automated mode for production work but switch to manual for one-off cuts and repairs. The control system allows quick switching between modes.


Hot Tags: compact plasma gantry cutter, China compact plasma gantry cutter manufacturers, factory, fiber laser cutting machine for metal, gantry laser cutting machine, handheld fiber laser welding and cutting machine, Heavy Duty Portable CNC Plasma Cutter, High Precision Portable CNC Plasma Cutter, Industrial Portable CNC Plasma Cutter


